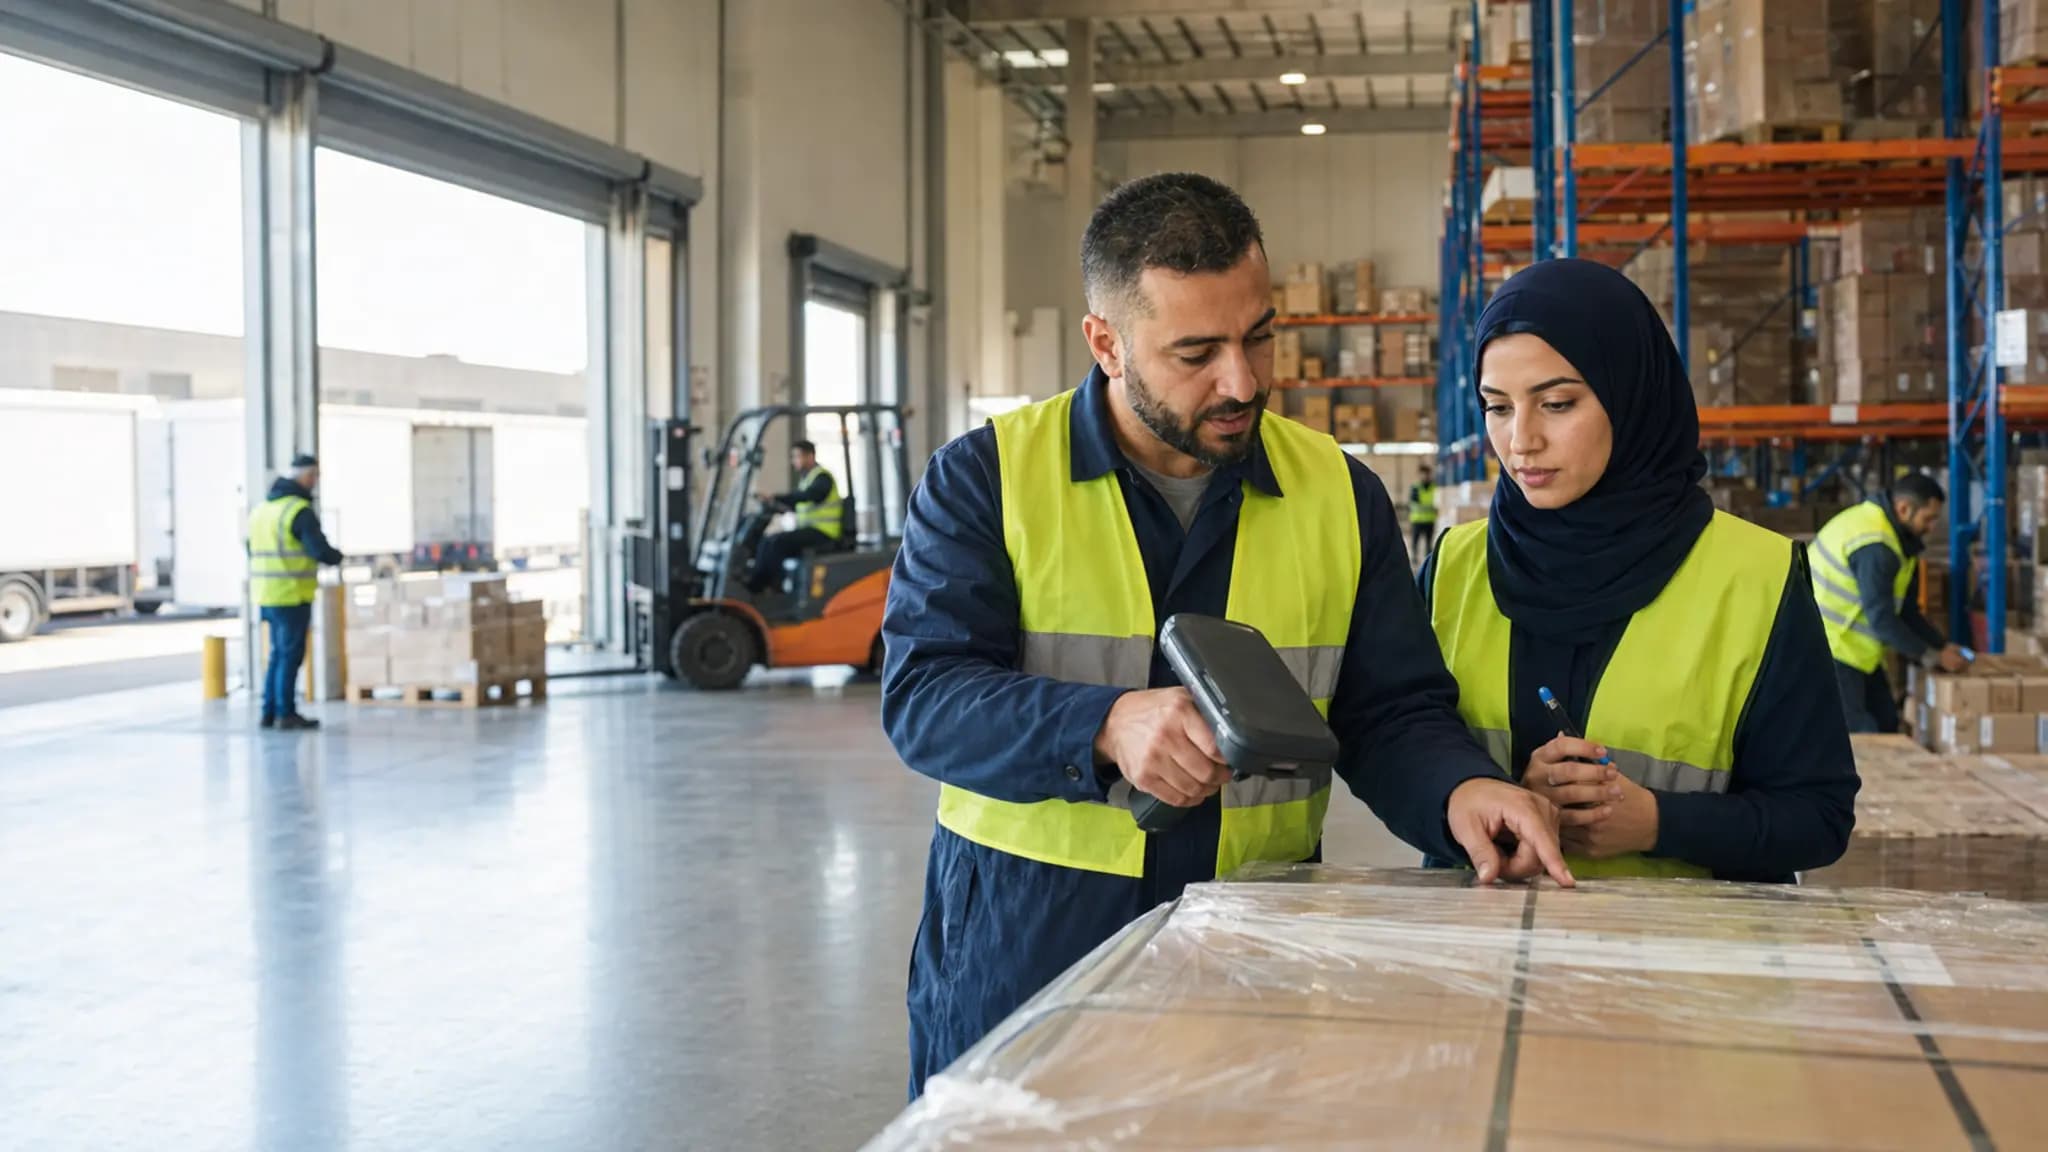
One sheet, one situation, one line of reasoning to practise.
Intended for business and engineering schools, logistics courses, and teams onboarding new colleagues.
This series does not attempt to cover warehouse logistics. It aims to give a student or new starter the six lines of reasoning needed to understand what they see when they enter a warehouse for the first time.
Sheet 1 — A warehouse is not a storage place
The situation
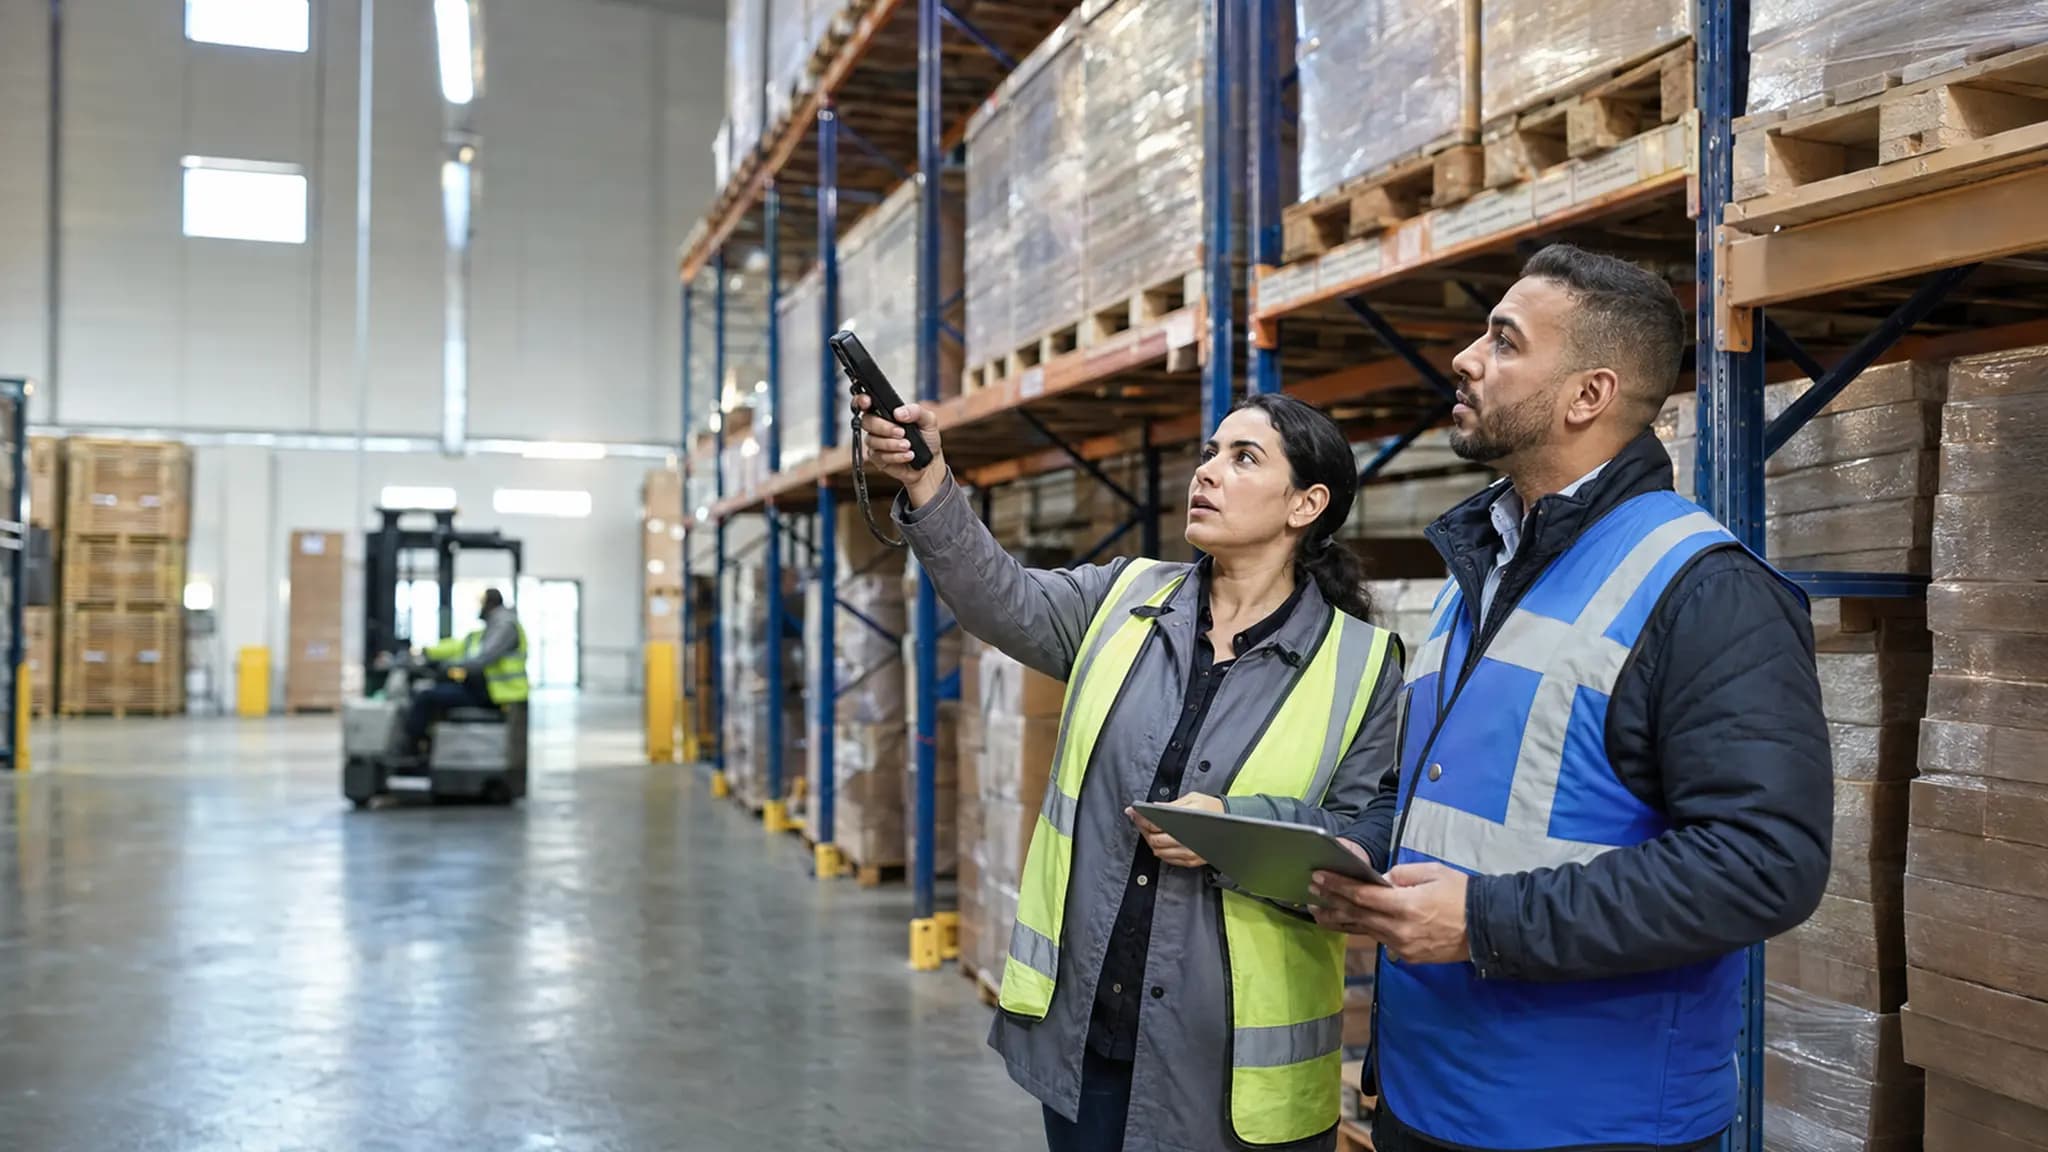
You enter a warehouse. You see full racking, aisles and forklifts. The temptation is to think: ‘this is a place where goods are kept’.
That is the most natural interpretation, and the one that prevents you from understanding everything else.
The reasoning
A warehouse is a synchronisation mechanism. It exists because the rate at which goods arrive is not the rate at which they are requested.
A supplier produces in batches of one thousand. A customer orders three at a time. A ship arrives once a month, while consumption is daily. A harvest takes place over six weeks, while sales extend over the year. The warehouse absorbs this difference in rhythm.
This definition has an immediate practical consequence: a warehouse’s performance is measured not by what it contains, but by its ability to keep things moving. A full warehouse is not a high-performing warehouse. It is often the opposite.
Common mistakes
Judging a warehouse by its fill rate. A high rate may mean efficient use of space — or stock that does not move.
Trying to maximise storage capacity without asking whether inbound and outbound flows can keep pace.
Forgetting that every additional square metre of storage creates extra work: more distance to travel, more items to check and more inventory to maintain.
Exercise
Observe or imagine a warehouse. Ask yourself three questions:
What arrives, at what rate and in what packaging?
What leaves, at what rate and in what packaging?
Exactly what difference between the two does the warehouse absorb?
The answer to the third question is the warehouse’s reason for being. Everything else — layout, equipment and organisation — follows from it.
Sheet 2 — The load unit determines everything
The situation
Two warehouses of the same size, storing products of comparable value, may have radically different organisations. The cause often lies in one variable: what is actually handled.
The reasoning
The load unit is what can be moved in one action: a full pallet, a case or an individual item by hand.
This unit determines, in sequence:
equipment — an 800 kg pallet is not handled with the same tools as a 4 kg case;
layout — usable height, aisle width and type of floor;
work organisation — picking full pallets, cases or individual units, which completely changes picking time;
the information system — the data to be tracked is not the same.
A single warehouse often combines several load units according to product or customer. That is legitimate, but every additional combination adds complexity — and that complexity has a cost that must be accepted consciously.
Common mistakes
Designing the layout for today’s dominant load unit without anticipating changes in ordering patterns. Many warehouses designed for pallets find themselves picking individual units in unsuitable aisles.
Neglecting out-of-gauge items, which occupy disproportionate space and break every rule.
Exercise
For three different products in the same warehouse, describe how each arrives, how it is stored and how it leaves. Then identify where the load unit changes (for example, a pallet broken down into cases). These break points are where errors concentrate.
Sheet 3 — Every location must have a name
The situation
Two warehouse operators look for the same product. The first, who has been with the company for eight years, heads straight to the aisle at the back. The second, who started on Monday, wanders for ten minutes.
The warehouse works — but it works because of one person’s memory, not because of its organisation.
The reasoning
Addressing means giving every storage position a unique, stable and readable identifier. It turns personal knowledge into shared information.
A good addressing scheme follows four principles:
uniqueness: two locations never have the same name;
stability: the name does not change when the warehouse is reorganised;
readability: the label can be read from the actual working position, including from a forklift at height;
route logic: numbering follows the direction of travel, so that ‘go from A-01 to A-12’ is one continuous movement.
Addressing is the prerequisite for any digitisation. At heart, an information system merely associates products with addresses.
Common mistakes
Assigning addresses on a plan without labelling them physically.
Labelling once, then reorganising without updating.
Choosing an overly rich naming convention in which the code describes the product type. The product changes location; the location name must not depend on what it contains.
Exercise
Propose an addressing convention for a warehouse with 5 aisles, 20 bays per aisle and 4 height levels. Then test it: write down three random addresses and check that an outsider can locate them without explanation.
Sheet 4 — Picking is the costliest activity
The situation
In most warehouses, order picking accounts for the largest share of working time. And within that share, walking often accounts for most of it.
The reasoning
Picking an order means moving through a warehouse to gather items. Time breaks down roughly into travelling, searching, picking, checking and packing.
Travel almost always dominates — and it is also the part that adds no value.
Hence the main levers, in the order in which they are used:
Place the most frequently requested items closest to the starting areas and at picking height. This is called slotting.
Group orders so that one journey serves several orders.
Sequence the route to avoid backtracking.
Replenish picking locations before they are empty — a stockout in picking costs far more than early replenishment.
These levers require no capital investment. They require knowledge of your outbound data.
Common mistakes
Optimising slotting once and never reviewing it. Item turnover changes; the layout must follow.
Grouping orders without planning a check: grouping multiplies the risk of mixing orders.
Measuring productivity in lines per hour without accounting for distance travelled, unfairly penalising pickers assigned to distant zones.
Exercise
Using a fictional list of 20 orders covering 10 items, propose a picking sequence. Compare two strategies: order by order, then grouped. Estimate the difference in distance travelled. Then identify the new risk introduced by grouping.
Sheet 5 — A stock variance is information, not a fault
The situation
A stocktake reveals that 12 units of an item are missing. The first, almost universal reaction is to look for someone responsible.
That is understandable, and the surest way never to solve the problem.
The reasoning
A stock variance is a symptom. It shows that, at some point, a physical movement was not recorded, or that a record did not match the actual movement.
The most common causes, in order:
a picking error — the adjacent item was taken, often because the packaging looks similar;
a poorly checked receipt — the variance already existed on entry and was discovered weeks later;
an unrecorded movement — an urgent relocation, undeclared breakage or a sample withdrawal;
a data-entry error — unit confused with case, decimal separator misplaced;
an actual loss — which does occur, but ranks after the other four in the statistics.
Looking for someone to blame focuses attention on the fifth cause and hides the first four, which are organisational problems.
Common mistakes
Adjusting stock without recording the reason. The symptom is erased and the information is lost.
Counting only once a year, making any investigation impossible: no one will ever know when the variance appeared.
Counting while knowing the expected quantity. The brain confirms what it expects to see; counting must be blind.
Exercise
For a variance on a given item, list five possible causes. Then, for each one, state what information would confirm or rule it out. You have just defined what an information system should trace.
Sheet 6 — What is not measured does not improve
The situation
A warehouse manager is asked whether the operation performs well. The answer is that ‘it runs smoothly’. Asked how they know, there is silence.
The reasoning
A useful indicator meets four conditions: it is linked to a decision that can be made, it can be measured without disproportionate effort, its definition is stable, and someone is accountable for its value.
An indicator that triggers no decision is a decorative figure.
The families of warehouse indicators:
Reliability — stock accuracy, time taken to detect a variance.
Service — complete orders, orders delivered within the promised time.
Productivity — volume processed per hour worked, provided the scope is specified.
Quality — picking errors, disputes, returns caused by an internal error.
Utilisation — occupancy by zone, dock saturation.
Three common-sense principles that are often forgotten:
Choose few indicators. Five tracked seriously are better than thirty displayed.
Adapt to the level. Management does not need the same figures as a team leader.
Measure before changing. Without a baseline, no improvement can be demonstrated.
Common mistakes
Publishing indicators without precisely defining their calculation. Two departments then calculate ‘service level’ differently, and the meeting focuses on the method rather than action.
Tracking indicators that no decision can influence.
Using indicators to assess people rather than processes — after which the figures, as everywhere, become optimised rather than accurate.
Exercise
Choose a concrete warehouse problem (for example, orders delivered incomplete). Propose a single indicator that would show whether the problem is worsening or improving. Define its calculation precisely: numerator, denominator, scope and frequency. Then identify who should own it.
Going further
These six sheets cover the basic reasoning. They replace neither a full course nor floor experience — logistics is learned by walking through a warehouse, not by reading.
Institutions wishing to use this series in an educational setting can contact us: we support several courses and are happy to contribute to real cases.
Educational series published by B-AGILE Systems. Reproduction permitted for teaching purposes, with acknowledgement of the source.